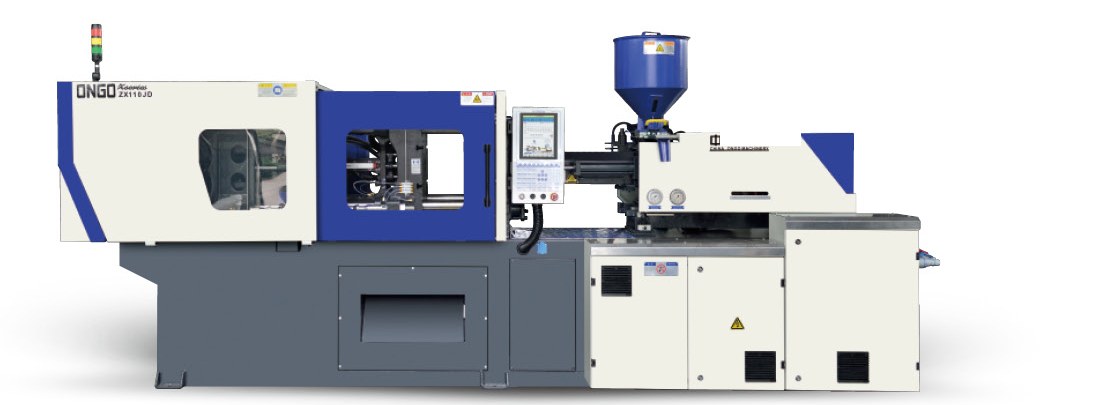
Servo-hydraulic machines from 1,100 to 29,000 kN — the range that covers general plastics, engineering plastics and PET packaging, with four screw configurations per model so the machine is sized to the part rather than the other way round.
The Z Series is split into four families by clamping force. Within each family, every model offers three or four screw configurations — the same machine can be set up for a 2,600 g shot at low pressure or a 3,500 g shot at high pressure, depending on the part.
| Family | Clamping force | Models | Typical applications |
|---|---|---|---|
| ZX110 – ZX270 | 1,100 – 2,700 kN | 5 | General plastics, small components, thin-wall packaging |
| ZX318 – ZX650 | 3,180 – 6,500 kN | 5 | General and engineering plastics, crates, buckets, automotive parts |
| Z700 – Z1300 | 7,000 – 13,000 kN | 5 | Large structural parts, pallets, thick-wall containers |
| Z1400 – Z2900 | 15,000 – 29,000 kN | 5 | Large automotive, heavy-duty packaging, thick structural parts |
| Z-PET series | 2,700 – 5,200 kN | 4 (9 variants) | PET preforms and bottles — mineral water, beverage, edible oil, household chemical |
Clamping force listed in kN. Divide by 9.81 for the tonnage equivalent — a Z1500 is roughly 1,500 tons. Machine selection should start from your part's projected area, not from a model name — see our machine sizing guide for the calculation.
These are not competing products at the same end of the market — they cover different needs. Here is where each one is genuinely the better answer.
A servo pump system fitted across the range delivers power on demand rather than running continuously. It cuts energy consumption considerably compared with a fixed-displacement hydraulic machine of the same size, without the purchase premium of a fully electric machine.
A one-piece linkage structure with high-quality copper bushes combines clamping rigidity and accuracy. This is what keeps platen parallelism within tolerance over years, and it is why platen parallelism on a used Z machine is worth checking on inspection.
The injection carriage uses an integral copper sleeve, giving stable plasticising and repeatable shot accuracy. Shot consistency is what determines dimensional consistency on the part, so this detail matters more than it sounds.
Each model offers A / B / C / D screw diameters, letting you balance shot weight against process pressure for the parts you actually run. This is the feature that lets one machine cover a product range instead of forcing a compromise on the screw.
| Standard configuration | Why it matters in production |
|---|---|
| Double-cylinder injection unit with injection-end cushion control | Stable cushion means stable shot weight, which means stable dimensions |
| High-performance flow-type injection structure, low-inertia carriage | Faster response and less energy per shot |
| Four-stage large-flow cartridge valve clamping system | Clamping force stays stable across the whole mould thickness range |
| Automatic mould height adjustment | Changeover without manual re-setting, fewer setup errors |
| Core pull, unscrewing, special nozzle, multi-point ejection reserved | Capability to add features later without replacing the machine |
| Bi-metal barrel with precision screw and IR melt temperature sensing | Wear resistance plus accurate melt temperature control |
| Automatic cooling water temperature control with alarm | Stable mould temperature, which is half of warpage control |
| Centralised lubrication with oil starvation alarm | Prevents the bearing damage that comes from running dry |
| PLC + TFT true-colour control, 60 mould parameter memory | Recall settings per mould rather than relying on someone remembering |
| Temperature deviation display, screw cold-start protection, electronic mould scale protection | Protects both machine and mould when something goes wrong |
Optional configuration
| Optional | When it is worth adding |
|---|---|
| PID multi-stage cavity / holding pressure control | Tight dimensional requirements, or a product with heavy thick-to-thin variation |
| Insulation plates and quick mould change device | High changeover frequency — the saving is in setup time |
| Robot, conveyor and automation interface with line control | Unattended running, or where labour is the constraint |
| Hopper dryer and dehumidifying conveying system | Any hygroscopic resin — see the drying guide |
| Servo plasticising motor, bi-alloy screw upgrade | Cycle time where recovery is the bottleneck, or abrasive resins |
| Corrosion / heat resistant screw and barrel sets | PVC, flame-retardant grades, engineering plastics |
| Oil temperature cooling and heating unit | Process control where melt temperature stability matters |
| Water manifold, low-pressure mould protection, automatic lubrication | Mould protection where a low-pressure mould is fitted |
| SPC and network data management interface | Where you need process data traceable to a customer requirement |
| Customised configurations for preforms, caps and thin-wall parts | When the standard configuration will not hold the target cycle |
Values below are for each screw configuration. Where a model has four configurations they are listed A through D. Shoot your part and we will confirm which configuration fits — this table is the reference, not a substitute for that calculation.
| Item | Unit | ZX110 A / B / C | ZX140 A / B / C | ZX170 A / B / C | ZX230 A / B / C | ZX270 A / B / C |
|---|---|---|---|---|---|---|
| Screw diameter | mm | 32 / 36 / 40 | 38 / 40 / 45 | 40 / 45 / 50 | 45 / 50 / 55 | 50 / 55 / 60 |
| Shot volume (theoretical) | cm³ | 137 / 173 / 214 | 227 / 251 / 318 | 283 / 358 / 442 | 397 / 491 / 594 | 530 / 641 / 763 |
| Injection weight (PS) | g | 124 / 157 / 194 | 206 / 229 / 289 | 257 / 325 / 402 | 362 / 446 / 540 | 482 / 583 / 694 |
| Injection rate | g/s | 78 / 99 / 122 | 107 / 119 / 150 | 124 / 158 / 194 | 169 / 209 / 252 | 217 / 263 / 313 |
| Injection pressure | MPa | 273 / 215 / 174 | 218 / 197 / 155 | 235 / 185 / 150 | 218 / 176 / 146 | 215 / 178 / 149 |
| Screw speed | rpm | 228 | 225 | 180 | 197 | 210 |
| Clamping force | kN | 1,100 | 1,400 | 1,700 | 2,300 | 2,700 |
| Open stroke | mm | 350 | 380 | 435 | 475 | 540 |
| Space between tie bars (W×H) | mm | 370 × 370 | 420 × 420 | 470 × 470 | 520 × 520 | 570 × 570 |
| Max. mould height | mm | 380 | 450 | 520 | 530 | 610 |
| Min. mould height | mm | 150 | 160 | 180 | 200 | 200 |
| Ejector stroke | mm | 102 | 121 | 140 | 142 | 150 |
| Ejector force | kN | 38 | 53 | 53 | 71 | 71 |
| Pump motor power (servo) | kW | 13.4 | 13.4 | 16.4 | 20.5 | 26.7 |
| Heating power | kW | 7.8 | 10.8 | 12.5 | 16.4 | 18.9 |
| Machine dimension (L×W×H) | m | 4.4 × 1.27 × 1.90 | 4.58 × 1.33 × 1.90 | 5.02 × 1.48 × 2.10 | 5.44 × 1.50 × 2.14 | 5.82 × 1.63 × 2.27 |
| Oil tank capacity | L | 160 | 175 | 210 | 230 | 270 |
| Machine weight | t | 3.4 | 4.0 | 6.0 | 7.0 | 8.0 |
| Item | Unit | ZX318 A / B / C | ZX360 A / B / C | ZX460 A / B / C | ZX530 A / B / C | ZX650 A / B / C / D |
|---|---|---|---|---|---|---|
| Screw diameter | mm | 55 / 60 / 65 | 65 / 70 / 75 | 70 / 75 / 80 | 75 / 80 / 85 | 90 / 95 / 100 / 105 |
| Shot volume (theoretical) | cm³ | 630 / 749 / 879 | 1,114 / 1,292 / 1,484 | 1,500 / 1,722 / 1,959 | 1,810 / 2,060 / 2,325 | 2,861 / 3,188 / 3,533 / 3,895 |
| Injection weight (PS) | g | 573 / 682 / 800 | 1,014 / 1,176 / 1,350 | 1,365 / 1,567 / 1,783 | 1,647 / 1,874 / 2,116 | 2,604 / 2,901 / 3,215 / 3,544 |
| Injection rate | g/s | 276 / 329 / 386 | 352 / 372 / 469 | 344 / 395 / 449 | 458 / 521 / 588 | 603 / 672 / 745 / 821 |
| Injection pressure | MPa | 211 / 178 / 151 | 207 / 179 / 156 | 212 / 185 / 162 | 204 / 179 / 159 | 177 / 159 / 143 / 130 |
| Screw speed | rpm | 218 | 205 | 162 | 142 | 107 |
| Clamping force | kN | 3,180 | 3,600 | 4,600 | 5,300 | 6,500 |
| Open stroke | mm | 660 | 660 | 740 | 800 | 870 |
| Space between tie bars (W×H) | mm | 620 × 620 | 670 × 670 | 770 × 770 | 830 × 820 | 880 × 880 |
| Max. mould height | mm | 660 | 720 | 780 | 810 | 900 |
| Min. mould height | mm | 220 | 250 | 250 | 250 | 350 |
| Ejector stroke | mm | 150 | 162 | 202 | 220 | 250 |
| Ejector force | kN | 71 | 71 | 113 | 152 | 150 |
| Pump motor power (servo) | kW | 31.1 | 50.7 | 50.7 | 60.5 | 31.1 + 31.1 |
| Heating power | kW | 24.8 | 28.6 | 32.2 | 34.4 | 49.9 |
| Machine dimension (L×W×H) | m | 6.46 × 1.6 × 2.16 | 7.21 × 1.85 × 2.34 | 8.11 × 1.95 × 2.41 | 8.35 × 2.1 × 2.7 | 10.2 × 2.15 × 2.6 |
| Oil tank capacity | L | 410 | 620 | 650 | 790 | 800 |
| Machine weight | t | 9.5 | 12.5 | 16 | 20 | 28 |
| Item | Unit | Z700 A / B / C / D | Z780 A / B / C / D | Z980 A / B / C | Z1100 A / B / C / D | Z1300 A / B / C / D |
|---|---|---|---|---|---|---|
| Screw diameter | mm | 90 / 95 / 100 / 105 | 90 / 95 / 105 / 110 | 90 / 100 / 110 | 100 / 110 / 120 / 130 | 110 / 120 / 130 / 140 |
| Shot volume (theoretical) | cm³ | 2,861 / 3,188 / 3,533 / 3,895 | 2,989 / 3,330 / 4,068 / 4,464 | 3,561 / 4,396 / 5,319 | 4,710 / 5,699 / 6,782 / 7,960 | 5,794 / 6,895 / 8,092 / 9,385 |
| Injection weight (PS) | g | 2,604 / 2,901 / 3,215 / 3,544 | 2,719 / 3,030 / 3,702 / 4,063 | 3,240 / 4,000 / 4,840 | 4,286 / 5,186 / 6,172 / 7,244 | 5,272 / 6,274 / 7,364 / 8,541 |
| Injection rate | g/s | 679 / 756 / 838 / 924 | 586 / 653 / 798 / 876 | 708 / 874 / 1,058 | 772 / 935 / 1,112 / 1,305 | 785 / 934 / 1,096 / 1,271 |
| Injection pressure | MPa | 177 / 159 / 143 / 130 | 195 / 176 / 144 / 131 | 215 / 174 / 144 | 207 / 171 / 144 / 123 | 201 / 169 / 144 / 124 |
| Screw speed | rpm | 120 | 115 | 115 | 128 | 93 |
| Clamping force | kN | 7,000 | 7,800 | 9,800 | 11,000 | 13,000 |
| Open stroke | mm | 980 | 950 | 1,115 | 1,250 | 1,420 |
| Space between tie bars (W×H) | mm | 960 × 940 | 980 × 980 | 1,080 × 1,080 | 1,170 × 1,170 | 1,280 × 1,280 |
| Max. mould height | mm | 940 | 960 | 1,080 | 1,220 | 1,350 |
| Min. mould height | mm | 350 | 400 | 500 | 500 | 600 |
| Ejector stroke | mm | 280 | 280 | 280 | 325 | 325 |
| Ejector force | kN | 210 | 210 | 210 | 245 | 245 |
| Pump motor power (servo) | kW | 31.1 + 50.7 | 31.1 + 50.7 | 31.1 + 50.7 | 31.1 + 31.1 + 50.7 | 31.1 + 31.1 + 50.7 |
| Heating power | kW | 49.9 | 56.3 | 68.1 | 69.1 | 74.3 |
| Machine dimension (L×W×H) | m | 10.2 × 2.3 × 2.7 | 10.7 × 2.26 × 2.91 | 11.43 × 2.4 × 2.96 | 12.4 × 2.79 × 3.16 | 13.1 × 2.92 × 3.16 |
| Oil tank capacity | L | 800 | 1,200 | 1,200 | 1,600 | 1,600 |
| Machine weight | t | 32 | 36 | 43 | 50 | 60 |
| Item | Unit | Z1500 A / B / C | Z1800 A / B / C / D | Z2300 A / B / C / D | Z2500 A / B / C / D | Z2900 A / B / C |
|---|---|---|---|---|---|---|
| Screw diameter | mm | 120 / 130 / 140 | 130 / 140 / 150 / 160 | 140 / 150 / 160 / 170 | 160 / 170 / 185 / 190 | 190 / 200 / 230 |
| Shot volume (theoretical) | cm³ | 7,122 / 8,258 / 9,693 | 9,021 / 10,462 / 12,011 / 13,665 | 11,847 / 13,600 / 15,473 / 17,469 | 21,101 / 23,820 / 28,209 / 29,755 | 34,006 / 37,680 / 49,831 |
| Injection weight (PS) | g | 6,481 / 7,606 / 8,821 | 8,209 / 9,521 / 10,930 / 12,435 | 10,780 / 12,376 / 14,081 / 15,896 | 19,201 / 21,677 / 25,671 / 27,077 | 30,946 / 34,289 / 45,347 |
| Injection rate | g/s | 944 / 1,108 / 1,285 | 987 / 1,145 / 1,314 / 1,495 | 1,039 / 1,193 / 1,357 / 1,532 | 1,272 / 1,436 / 1,701 / 1,794 | 1,472 / 1,631 / 2,157 |
| Injection pressure | MPa | 193 / 164 / 142 | 184 / 159 / 138 / 122 | 201 / 175 / 154 / 137 | 219 / 194 / 164 / 156 | 190 / 171 / 129 |
| Screw speed | rpm | 91 | 70 | 60 | 60 | 70 |
| Clamping force | kN | 15,000 | 18,000 | 23,000 | 25,000 | 29,000 |
| Open stroke | mm | 1,500 | 1,600 | 1,870 | 1,960 | 2,030 |
| Space between tie bars (W×H) | mm | 1,480 × 1,360 | 1,580 × 1,480 | 1,800 × 1,620 | 1,870 × 1,710 | 2,050 × 1,760 |
| Max. mould height | mm | 1,500 | 1,600 | 1,700 | 1,800 | 1,900 |
| Min. mould height | mm | 700 | 650 | 700 | 700 | 700 |
| Ejector stroke | mm | 375 | 400 | 400 | 450 | 450 |
| Ejector force | kN | 282 | 407 | 565 | 565 | 565 |
| Pump motor power (servo) | kW | 50.7 + 50.7 + 50.7 | 50.7 + 50.7 + 50.7 + 50.7 | 50.7 + 50.7 + 50.7 + 50.7 | 50.7 × 4 or × 5 | 50.7 + 50.7 + 50.7 |
| Heating power | kW | 101.1 | 106.7 | 126.2 | 199.9 | 220 |
| Machine dimension (L×W×H) | m | 14.1 × 3.2 × 3.5 | 16.35 × 3.62 × 3.58 | 18.3 × 4.0 × 3.78 | 18.8 × 4 × 4.4 | 21 × 4.2 × 4.5 |
| Oil tank capacity | L | 1,800 | 2,400 | 2,600 | 2,600 | 3,640 |
| Machine weight | t | 80 | 120 | 150 | 180 | 210 |
| Item | Unit | Z270PET | Z360PET | Z460PET | Z520PET |
|---|---|---|---|---|---|
| Variant — injection unit | g | 1,400 | 3,000 / 5,000 | 3,500 / 5,000 | 5,000 / 11,000 |
| Screw diameter | mm | 65 | 85 / 110 | 95 / 110 | 110 / 130 |
| Screw L/D ratio | L/D | 24 | 25 | 25 | 25 / 26 |
| Shot volume (theoretical) | cm³ | 978 | 2,212 / 5,224 | 2,833 / 5,224 | 5,224 / 9,286 |
| Injection weight (PET) | g | 1,124 | 2,545 / 6,007 | 3,258 / 6,007 | 6,007 / 10,679 |
| Injection rate | g/s | 394 | 625 / 1,037 | 815 / 1,037 | 1,037 / 1,534 |
| Injection pressure | MPa | 143 | 134 / 101 | 118 / 101 | 101 / 123 |
| Screw speed | rpm | 130 | 120 / 95 | 105 / 95 | 95 / 80 |
| Clamping force | kN | 2,700 | 3,000 | 3,200 | 5,200 |
| Open stroke | mm | 540 | 660 | 740 | 800 |
| Space between tie bars (W×H) | mm | 570 × 570 | 690 × 690 | 790 × 790 | 830 × 820 |
| Max. mould height | mm | 550 | 720 | 780 | 810 |
| Min. mould height | mm | 250 | 300 | 350 | 350 |
| Ejector stroke | mm | 150 | 182 | 182 | 220 |
| Ejector force | kN | 102 | 150 | 150 | 212 |
| Max. pump pressure | MPa | 16 | 16 | 16 | 16 |
| Pump motor power | kW | 36.7 | 41 | 51 | 41 + 41 |
| Heating power | kW | 26 | 37 | 52.4 | 75 |
| Plasticizing servo motor | kW | Optional | 50 / 60 | 60 | 92 |
| Machine dimension (L×W×H) | m | 6.5 × 1.6 × 2.2 | 8.9 × 1.8 × 2.2 | 9.5 × 1.9 × 2.1 | 10 × 2.1 × 2.8 |
| Oil tank capacity | L | 380 | 620 | 620 | 900 |
| Machine weight | t | 9 | 15.5 | 17.5 | 25 |
Suitable for PET packaging products such as mineral water, beverage, edible oil and household chemical bottles. Larger injection unit sizes are available on request. The 16 MPa pump pressure is what allows injection through the preform neck — this is the specific reason a standard Z machine is the wrong choice for PET, and it is also why drying is non-negotiable in PET work. See our drying guide for the PET drying cycle.
Specifications subject to change without notice. Injection weight is given for PS unless marked otherwise. Shot volume is theoretical. Values depend on the screw configuration shown — each figure above corresponds to the configuration in the same position.
Part drawing or finished part weight, resin, annual volume, target cycle, destination port. For PET, the bottle size and preform weight.
Clamping force calculated from your projected area, and the screw configuration chosen against your shot weight and required pressure — not rounded up to the biggest option.
Machine model, screw configuration, standard and optional configuration, price, lead time and shipping terms — all in writing before anything starts.
Manufacture, then more than 72 hours of continuous reliability testing with each key component recorded. Third-party inspection available at this stage.
Export packing, FOB or CIF to your port, documentation and tracking sent before the container departs.
Technical support on commissioning, spare parts supply, and wear parts matched to the screw configuration we fitted.
Machine size is calculated from your part's projected area at the required filling pressure, with a safety factor — not rounded up to the next frame. Screw configuration is specified against your shot weight and resin rather than supplied as a default. Every machine runs more than 72 hours of continuous reliability testing before delivery, with each key component recorded. Third-party inspection is available on request, and you are welcome to send your own inspector.
Tell us the part, the resin, the volume and your destination port. We will come back with the clamping force calculation, the screw configuration and the price — usually within 4 hours on business days.